Professional chicken cage manufacturers provide the essential infrastructure for modern poultry farming, focusing on high-efficiency housing systems that maximize space and bird health. These manufacturers specialize in integrating structural durability with automated biological requirements to ensure sustainable egg production and livestock management.
The shift toward industrial-scale poultry farming has introduced significant challenges, including labor shortages, disease control, and the need for precision egg collection. Without professional equipment, farms often struggle with high egg breakage rates and inefficient waste management, which directly impact the overall return on investment (ROI).
This guide analyzes the technical specifications and procurement standards of poultry housing systems, helping farm operators understand how to select equipment that balances automation with animal welfare. We will explore the working principles of automatic collection systems and the critical factors that distinguish top-tier manufacturers from generic suppliers.

1Understanding Modern Poultry Housing Systems

Modern poultry housing is no longer just about containment; it is a complex engineering environment designed to optimize the biological output of the flock. Leading chicken cage manufacturers utilize galvanized steel and high-density polymers to create environments that resist corrosion from ammonia and moisture, common in high-density poultry sheds.
These systems are typically categorized by tier counts—usually 3, 4, or 5 tiers—depending on the available ceiling height and the desired bird density. Each tier is engineered to facilitate natural movement while ensuring that waste is efficiently removed via conveyor systems to maintain air quality.
The integration of environmental control systems, such as automated ventilation and temperature regulation, works in tandem with the cage structure to reduce bird stress and maximize egg-laying consistency across the entire flock.
2Core Technical Specifications of Professional Cages
When analyzing equipment from top chicken cage manufacturers, the focus is on structural integrity and precision components. Frame materials typically consist of hot-galvanized steel sheets (often 3mm thick) to ensure the system can support the weight of thousands of birds without sagging or warping over time.
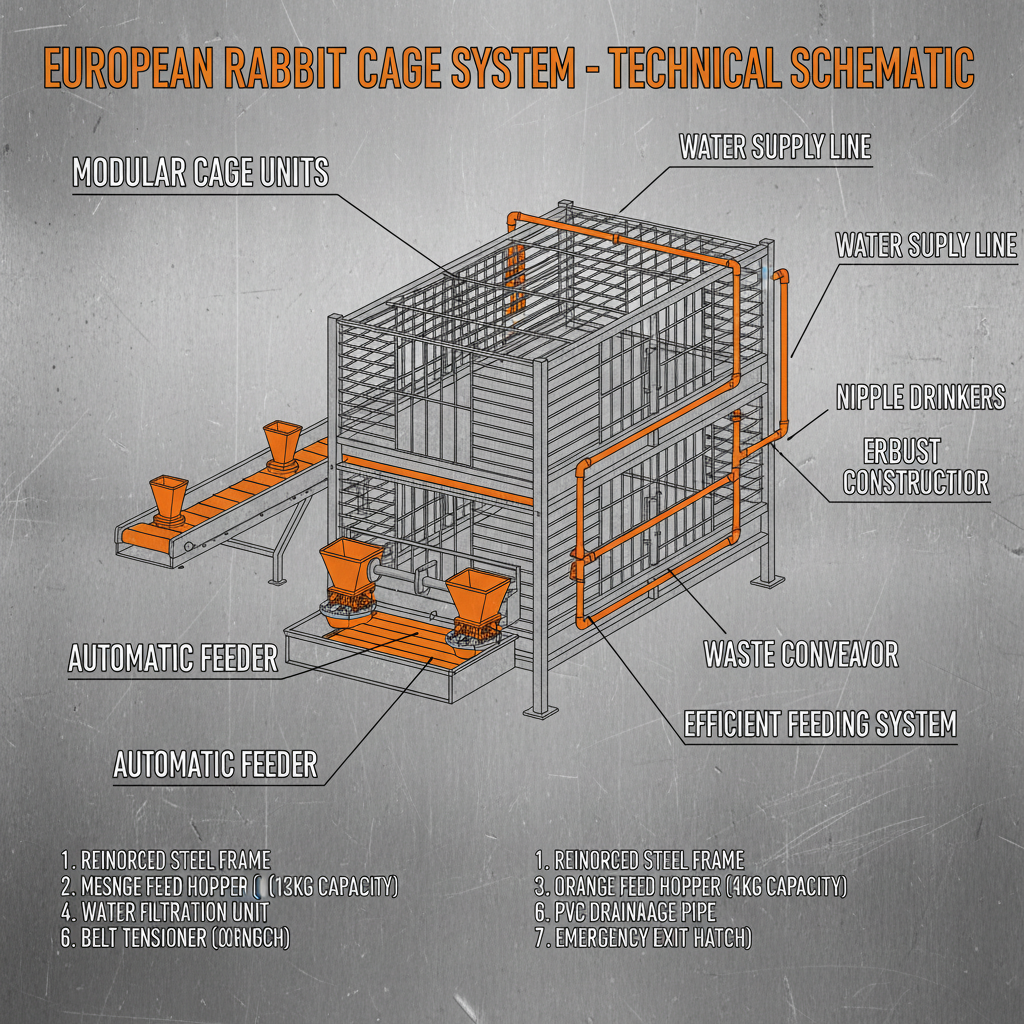
Feeding and watering systems are integrated directly into the cage frame. Nipple drinkers with pressure regulators ensure a constant water supply while minimizing spillage, which is crucial for keeping the bedding dry and reducing the risk of foot infections among the poultry.
The spacing and angle of the cage floors are mathematically calculated to encourage eggs to roll gently toward the collection belt, reducing the physical impact and subsequent breakage rate during the initial lay.
3Operational Workflow: Automatic Egg Collection
The automatic egg picking machine represents a significant leap in agricultural technology. The process begins with sensor-based detection; as an egg enters the collection tray, a sensor triggers the handling device. This prevents the need for manual inspection of every cage, saving hundreds of labor hours per month.
Once detected, a conveyor belt—typically 95mm to 100mm wide—transports the eggs from the front of the chicken shed to a centralized collection room. This intensive transport method ensures that eggs are moved in a streamlined fashion, minimizing human contact and the risk of pathogen spread.
This automation not only improves efficiency but also ensures that eggs are collected at a consistent frequency, which prevents eggs from being broken by the birds themselves or becoming soiled by waste.
4Comparative Performance: Manual vs. Automated
The transition from manual egg collection to automated systems provided by professional chicken cage manufacturers leads to a measurable decrease in operational overhead. Manual collection is prone to human error, inconsistency, and higher breakage rates due to improper handling.
Automated systems optimize the "egg-to-warehouse" timeline, ensuring that the product remains fresh and hygienic. By removing the need for workers to walk through the sheds constantly, the stress levels of the hens are lowered, which often results in improved laying rates.
chicken cage manufacturers Performance Metrics
As shown in the performance metrics, the most significant gains are seen in labor cost reduction and hygiene improvement. While the initial investment is higher, the reduction in egg breakage alone can provide a rapid return on investment for medium-to-large scale operations.
5Procurement Guide for Industrial Cage Systems
Procuring a system from chicken cage manufacturers requires a detailed understanding of your facility's dimensions and bird capacity. One must first determine the tier requirement (3, 4, or 5) based on the vertical space available and the structural load capacity of the building floor.
Compatibility is another key factor. Ensure that the automatic egg collection belts and feed troughs are compatible with your existing feed processing machines and environmental control equipment to create a seamless operational loop.
Finally, consider the scalability of the system. Modular designs allow farmers to expand their flock size by adding more cage sections without needing to overhaul the entire centralized collection infrastructure.
6Maintenance Constraints and Long-term Care
Despite the durability of high-end equipment, long-term success depends on a rigorous maintenance schedule. The conveyor belts and egg hooks are the most common points of wear. Regular inspection of the nylon hooks is necessary to prevent them from becoming brittle or misaligned.
Lubrication of the motor systems and the cleaning of the sensor eyes are critical. Dust and feathers can accumulate on the sensors, leading to "missed" eggs or false triggers, which disrupts the flow of the automatic collection process.
Operators should maintain a stock of spare parts, including egg claws and rollers, to ensure that any mechanical failure can be repaired within hours, preventing a backlog of eggs in the cages.
7Selecting the Right Manufacturer for Your Scale
Choosing between different chicken cage manufacturers depends on whether you require a standardized "off-the-shelf" solution or a customized ODM/OEM design. For large-scale industrial farms, customized layouts that optimize the movement of eggs and feed are essential for efficiency.
The reputation of the manufacturer in terms of after-sales service and certification (such as ISO9001) provides a layer of security, ensuring that the equipment meets international safety and quality standards.
| System Type | Best Use Case | Main Strength | Primary Limitation |
|---|---|---|---|
| 3-Tier Basic | Small-scale farms | Low initial cost | Lower space efficiency |
| 5-Tier Advanced | Industrial complexes | Maximum density | Requires high ceilings |
| Fully Automated | High-volume export | Minimal labor | Higher maintenance complexity |
| Semi-Automated | Growing enterprises | Balanced ROI | Some manual oversight needed |
| Modular Systems | Expanding farms | Flexible growth | Higher per-unit cost |
| Custom OEM | Specialized breeds | Perfect fit | Longer lead times |
Ultimately, the decision should be based on a total cost of ownership (TCO) analysis, weighing the initial purchase price against the projected savings in labor and the reduction in egg loss over a 10-year lifecycle.
Frequently Asked Questions
Conclusion
Selecting high-quality equipment from experienced chicken cage manufacturers is a strategic decision that defines the efficiency and hygiene of a poultry operation. By focusing on structural durability, such as galvanized steel, and embracing automation through egg collection systems, farmers can significantly reduce labor costs and improve product quality.
For operators looking to modernize their facilities or scale their production, reviewing detailed technical specifications and compatibility is essential. More information on available poultry solutions and equipment can be found at www.yizemachine.com.